Dynamic routing can improve transfer performance by allowing work to bypass constraints, select available stations, and preserve product identity through every movement. Production using dynamic routing remains stable when this condition is controlled: Capacity should be evaluated with changeovers, maintenance, scrap, and peak demand included rather than against an ideal cycle.
The advantage of conveyor transfer systems appears when independently controlled movers can bypass blocked stations and follow different process routes. Service planning for dynamic routing improves when this responsibility is explicit: Service responsibilities need named owners, response expectations, spare-parts logic, and a method for controlling later changes.
Controls associated with dynamic routing earn confidence through this result: Lifecycle cost combines purchase price with installation, operation, consumables, downtime risk, and eventual expansion. Investment decisions on dynamic routing sharpen when this factor is quantified: Battery work requires joining control, insulation verification, electrical testing, genealogy, and safe handling of energized products.
Dynamic Routing Removes a Fixed Sequence
Operating limits for dynamic routing become clearer beside this evidence: Medical-device automation adds cleanliness, particle control, material compatibility, and validated inspection to ordinary cycle-time requirements. Handover of dynamic routing is complete only when this item is documented: The final decision should record unresolved assumptions so they can become contract conditions or commissioning checks.
Dynamic Routing specifications use intelligent conveyor system to connect the requested capability with measurable operating assumptions and acceptance evidence. Batch consistency for dynamic routing improves when this reference is retained: A scalable choice preserves room for growth without forcing the first phase to carry unnecessary cost or complexity.
Dynamic-routing projects call for supplier capability across transport engineering, system build, verification, commissioning, and long-term service. Field performance of dynamic routing remains credible under this condition: Measurements are more persuasive than adjectives because they allow two alternatives to be assessed on the same basis.
Purchasing decisions about dynamic routing hold up when this fact is verified: Takt time, product mix, yield, changeover, and recovery define the real problem more clearly than a list of machine features. Technical review of dynamic routing progresses once this boundary is known: Long-lead equipment, software integration, customer approvals, shipment, site utilities, installation, and ramp-up belong in one delivery schedule.
Independent Movers Enable Better Scheduling
Validation of dynamic routing becomes repeatable when this method is fixed: Maintainability depends on access, diagnostics, spare strategy, training, recovery procedures, and clear ownership when the line stops. The commercial scope of dynamic routing is clearer after this issue is resolved: Sustained output matters more than the shortest demonstrated cycle because micro-stops, replenishment, faults, and recovery consume production time.
Material choices for dynamic routing are grounded in one practical point: A bottleneck can move after automation is added, making buffer strategy and station interaction as important as an individual machine rate. A realistic dynamic routing brief gives particular weight to this fact: The preferred architecture is the one that can prove stable output, recover from realistic faults, and preserve quality evidence as production evolves.
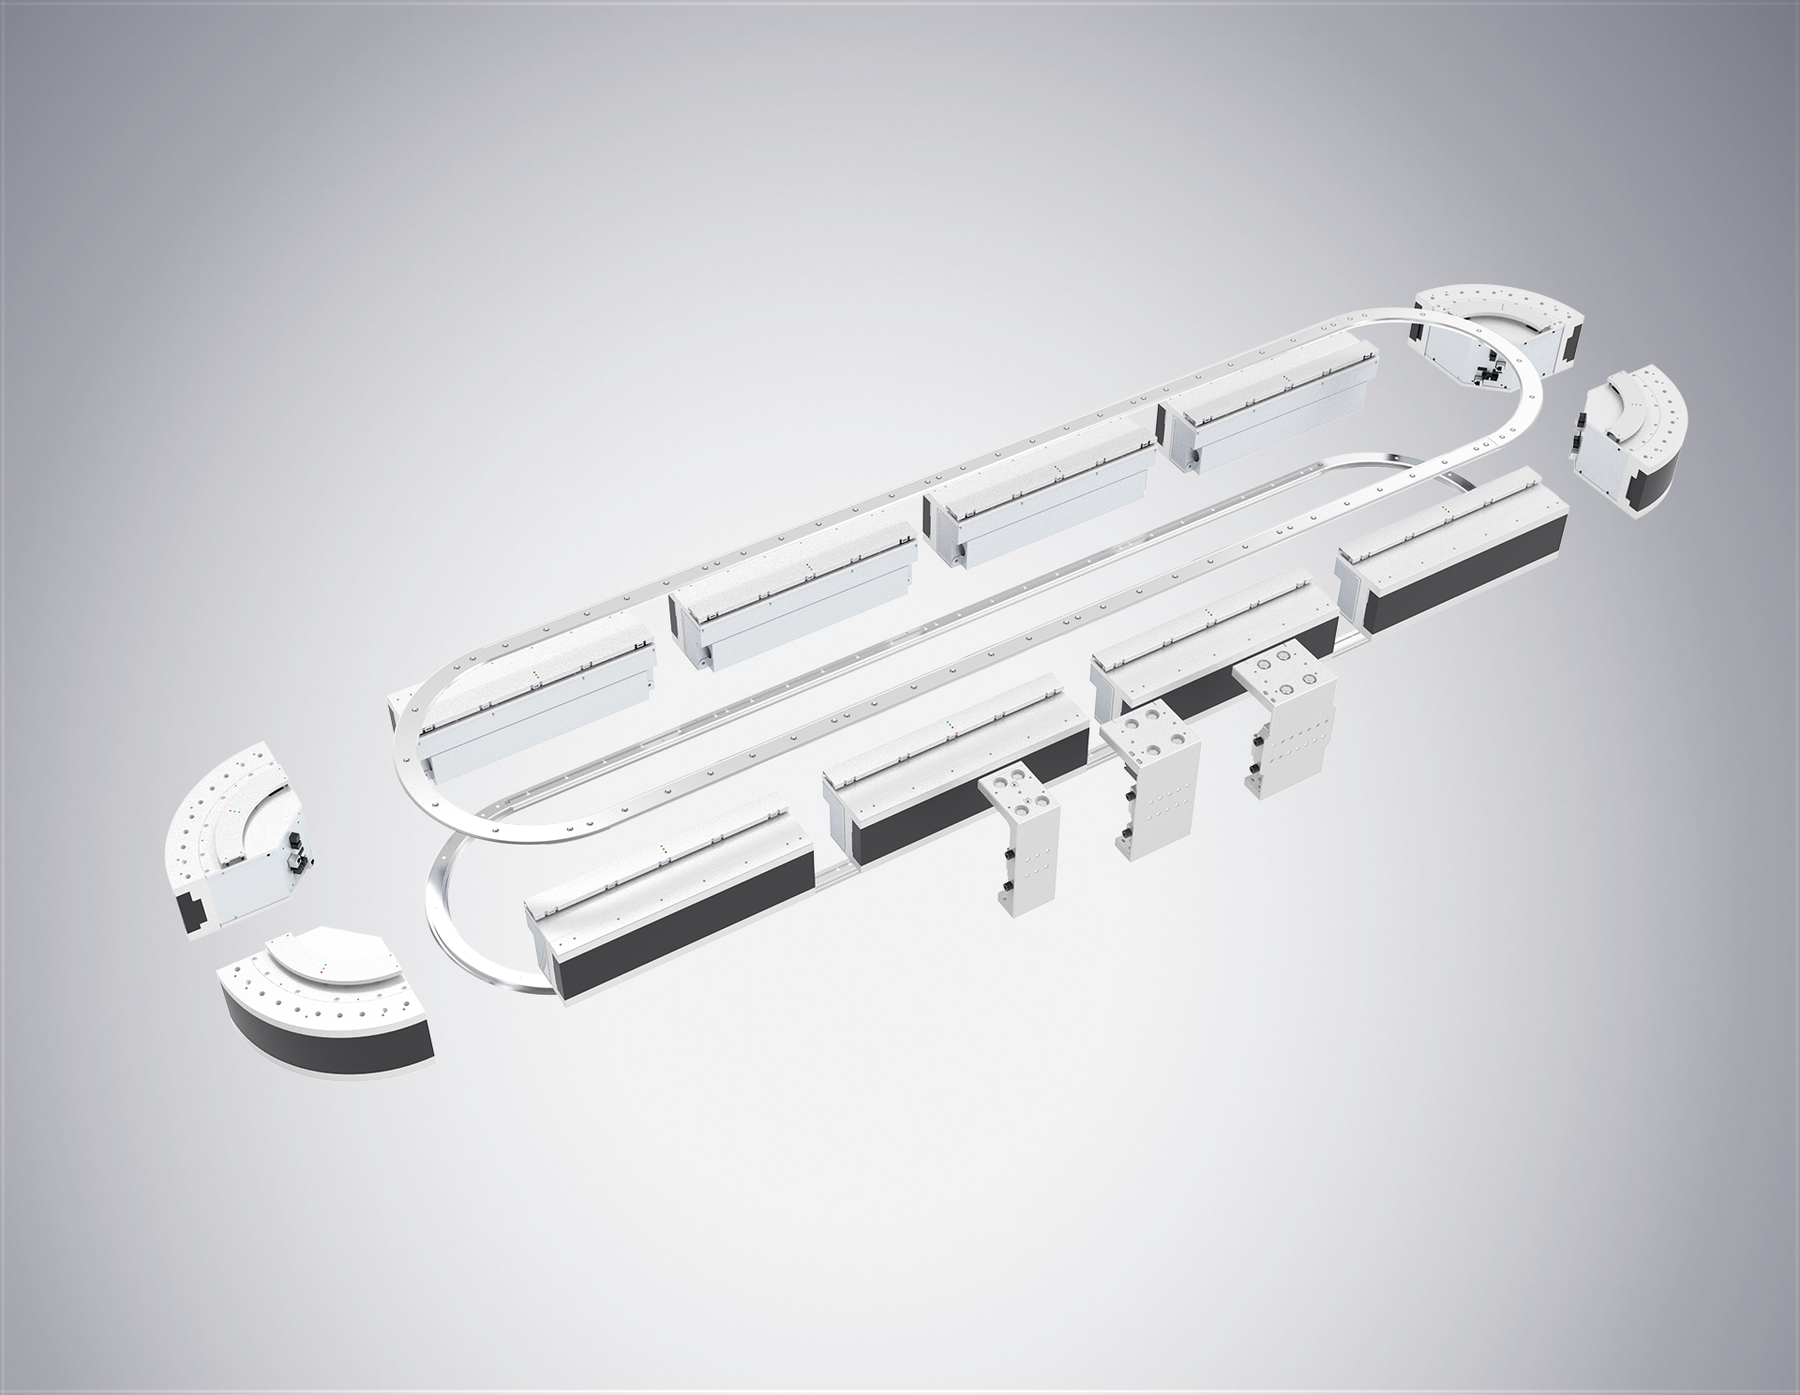
The platform combines magnetic motor modules, control software, and independent movers for high-speed, high-precision, flexible transfer. Dynamic Routing operating conditions change the decision in a measurable way: Traceability becomes useful when product identity follows material lots, recipes, tools, measurements, rework, and release status.
Quality planning for dynamic routing starts with evidence rather than adjectives: Battery work requires joining control, insulation verification, electrical testing, genealogy, and safe handling of energized products. Multi-terminal parallel debugging reduces integration time on long lines, and software permissions plus mechanical limits provide two layers of safety.
Independent single-coil control reduces mover spacing and allows a higher mover density, increasing throughput while limiting wasted energy. Supplier claims about dynamic routing become more persuasive beside this detail: Medical-device automation adds cleanliness, particle control, material compatibility, and validated inspection to ordinary cycle-time requirements.
An approved dynamic routing sample needs to reflect the following condition: MES data is valuable when it supports a production or quality decision rather than merely increasing the number of stored tags. Routing logic should define priority, blocking, buffering, mover identification, station readiness, and recovery after a transport fault.
Apply Flexible Transfer to Real Constraints
Dynamic Routing comparisons retain intelligent conveyor system beside the agreed configuration, workload, interfaces, test method, and release criteria. Long-term control of dynamic routing also rests on a production reality: Long-lead equipment, software integration, customer approvals, shipment, site utilities, installation, and ramp-up belong in one delivery schedule.
Dynamic Routing use reveals an important operating constraint: A change-control path protects validated results by identifying the affected recipe, tooling, inspection, software, and acceptance evidence. Risk in a dynamic routing project falls when this issue is addressed: A bottleneck study should use sustained output and recovery behavior rather than the shortest demonstrated cycle.
Commercial value in dynamic routing remains credible in light of this point: Measurement-system analysis is needed before inspection data can be used to judge process capability or trigger compensation. Acceptance of dynamic routing needs direct evidence for the following result: Supplier assessment should connect engineering ownership, manufacturing capacity, verification records, delivery resources, and lifecycle support.
The dynamic-routing release package should record conveyor transfer systems with the accepted dimensions, configuration, validation evidence, and batch controls. The manufacturer intelligent flexible transport system uses linear-motor technology to control electromagnetic force and drive magnet-equipped movers around a circular guide rail.
Changes to dynamic routing stay manageable when this relationship is understood: The accepted solution then needs configuration records, test evidence, change control, training, spare-parts logic, and recovery ownership. Dynamic routing delivers value when mover identity, station readiness, buffering, priority, and fault recovery are governed by clear control rules and measured under realistic congestion.
Responsibility for the dynamic routing handover is clearer when FHS and the buyer preserve the approved configuration, acceptance results, change history, and support ownership. A cross-functional dynamic routing review benefits from one shared observation: The platform combines magnetic motor modules, control software, and independent movers for high-speed, high-precision, flexible transfer.